Tubewell Steel & Engg. Co. is a leading manufacturer and stockist specializing in Alloy Steel Pipes, Tubes, Fittings and Flanges for critical industrial applications.
Tungsten-strengthened 9Cr-0.5Mo-1.8W-V-Nb seamless pipes for ultra-supercritical main steam and reheat piping at the highest temperatures.
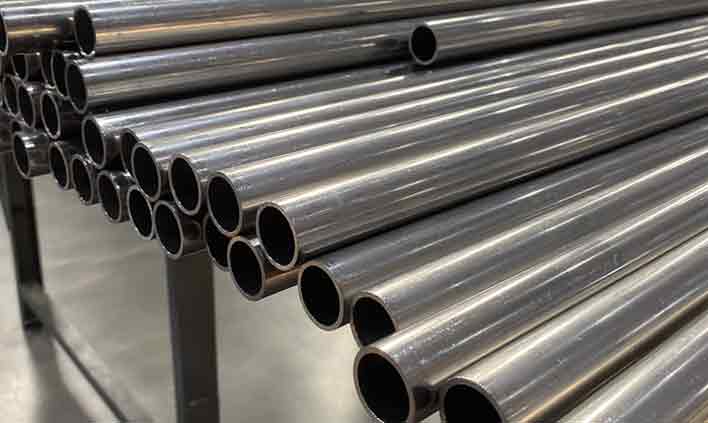
Tubewell Steel & Engg. Co. manufactures and stocks ASTM A335 P92 pipes – a 9Cr steel in which part of the molybdenum is replaced by about 1.8% tungsten, with micro-additions of vanadium, niobium, nitrogen and boron. P92 offers roughly 25–30% higher creep-rupture strength than P91 at 600–650°C, allowing thinner walls in ultra-supercritical power plants.
Next-generation 9Cr steel for ultra-supercritical steam conditions
ASTM A335 P92 (originally developed as NF616) is a seamless 9Cr-0.5Mo-1.8W-V-Nb alloy steel pipe from the creep strength enhanced ferritic family. Tungsten (1.50–2.00%) provides strong solid-solution strengthening, while vanadium, niobium and nitrogen form stable MX carbonitrides and a controlled boron addition (0.001–0.006%) stabilises M23C6 carbides at grain boundaries. Together these mechanisms give P92 the highest long-term creep strength of the A335 ferritic grades, with the oxidation resistance of 9% chromium.
Like P91, P92 depends on precise heat treatment: our pipes are normalized at 1040–1080°C and tempered at 730–800°C to a fully tempered martensitic structure, with hardness controlled to a maximum of 250 HBW. Each length is supplied with full heat traceability, 100% PMI, EN 10204 3.1 / 3.2 certificates, IBR Form III-A on request and third-party inspection by BV, TÜV, SGS, Lloyd's or EIL.
Standard supply range for ASTM A335 P92 pipes
| Parameter | Details |
|---|---|
| Standard | ASTM A335, ASME SA335 |
| Grade | P92 (UNS K92460) |
| Type | Seamless – Hot Finished / Cold Drawn |
| Size (NB) | 1/2" NB to 24" NB |
| Outer Diameter | 21.3 mm to 610 mm |
| Wall Thickness | SCH 80, 100, 120, 140, 160, XXS and heavy-wall MWT |
| Length | Single Random, Double Random, Cut Length (up to 12 m) |
| Ends | Plain End, Bevelled End (ASME B16.25) |
| Heat Treatment | Normalized 1040–1080°C (1900–1975°F) + Tempered 730–800°C (1350–1470°F) |
| Hardness | 250 HBW max |
| ASME P-Number | P-No. 15E, Group 1 |
| Dimension Standard | ASME B36.10M |
| Testing | Hydrostatic, Ultrasonic, Eddy Current, Flattening, Hardness, Micro-structure, PMI |
| Certificates | EN 10204 3.1 / 3.2, IBR Form III-A, TPI Reports |
International equivalents of A335 P92
| Standard | ASTM | UNS | EN | DIN / W.Nr. | JIS | Other |
|---|---|---|---|---|---|---|
| P92 | A335 P92 | K92460 | X10CrWMoVNb9-2 | 1.4901 | STPA 29 | NF616 |
Weight %, as per ASTM A335 (Ti ≤ 0.01, Zr ≤ 0.01)
| Grade | C | Mn | P | S | Si | Cr | Mo | W | V | Nb | N | B | Ni | Al |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| A335 P92 | 0.07 – 0.13 | 0.30 – 0.60 | 0.020 max | 0.010 max | 0.50 max | 8.50 – 9.50 | 0.30 – 0.60 | 1.50 – 2.00 | 0.15 – 0.25 | 0.04 – 0.09 | 0.030 – 0.070 | 0.001 – 0.006 | 0.40 max | 0.02 max |
Minimum values at room temperature, normalized & tempered condition
| Grade | Tensile Strength | Yield Strength (0.2%) | Elongation (Long.) | Elongation (Trans.) | Hardness |
|---|---|---|---|---|---|
| A335 P92 | 620 MPa (90 ksi) min | 440 MPa (64 ksi) min | 20% min | 13% min | 250 HBW max |
Typical values (for reference)
| Property | Metric | Imperial |
|---|---|---|
| Density | 7.85 g/cm³ | 0.284 lb/in³ |
| Melting Range | 1420 – 1500 °C | 2590 – 2730 °F |
| Modulus of Elasticity | 218 GPa | 31.6 × 10³ ksi |
| Thermal Conductivity (100°C) | 26 W/m·K | 15.0 BTU/h·ft·°F |
| Mean Thermal Expansion (20–300°C) | 11.0 µm/m·°C | 6.1 µin/in·°F |
| Specific Heat | 0.45 J/g·°C | 0.11 BTU/lb·°F |
| Max. Service Temperature | ≈ 650 °C | ≈ 1200 °F |
As per ASME B36.10M – heavy-wall schedules, wall thickness (mm) / weight (kg/m)
| NPS | OD (mm) | SCH 80 WT | SCH 80 Wt | SCH 160 WT | SCH 160 Wt | XXS WT | XXS Wt |
|---|---|---|---|---|---|---|---|
| 1/2" | 21.3 | 3.73 | 1.62 | 4.78 | 1.95 | 7.47 | 2.55 |
| 3/4" | 26.7 | 3.91 | 2.20 | 5.56 | 2.90 | 7.82 | 3.64 |
| 1" | 33.4 | 4.55 | 3.24 | 6.35 | 4.24 | 9.09 | 5.45 |
| 1 1/4" | 42.2 | 4.85 | 4.47 | 6.35 | 5.61 | 9.70 | 7.77 |
| 1 1/2" | 48.3 | 5.08 | 5.41 | 7.14 | 7.25 | 10.15 | 9.56 |
| 2" | 60.3 | 5.54 | 7.48 | 8.74 | 11.11 | 11.07 | 13.44 |
| 2 1/2" | 73.0 | 7.01 | 11.41 | 9.53 | 14.92 | 14.02 | 20.39 |
| 3" | 88.9 | 7.62 | 15.27 | 11.13 | 21.35 | 15.24 | 27.68 |
| 4" | 114.3 | 8.56 | 22.32 | 13.49 | 33.54 | 17.12 | 41.03 |
| 6" | 168.3 | 10.97 | 42.56 | 18.26 | 67.56 | 21.95 | 79.22 |
| 8" | 219.1 | 12.70 | 64.64 | 23.01 | 111.27 | 22.23 | 107.92 |
| 10" | 273.1 | 15.09 | 95.98 | 28.58 | 172.33 | 25.40 | 155.15 |
| 12" | 323.9 | 17.48 | 132.05 | 33.32 | 238.76 | 25.40 | 186.97 |
WT = Wall Thickness in mm, Wt = Weight in kg/m. Values are nominal; actual weights may vary within ASTM tolerances. Sizes 14" – 24" and minimum-wall (MWT) pipes supplied on request.
Where ASTM A335 P92 pipes are used
Main steam and hot reheat lines at 600°C+ steam temperature.
Thick-walled superheater and reheater outlet headers.
High-pressure, high-temperature combined-cycle steam piping.
Life-extension and uprating projects replacing older P22 / P91 lines.
High-temperature steam piping in CSP and thermal storage plants.
Severe high-temperature, high-pressure process piping.
Quality you can verify on every heat
Large inventory for fast dispatch
MTC EN 10204 3.1 / 3.2
Positive material identification
Pan-India & export shipping
Quick answers about A335 P92 pipes
Get competitive pricing, ready stock and complete documentation.